Not every elevator operates in a conventional building.
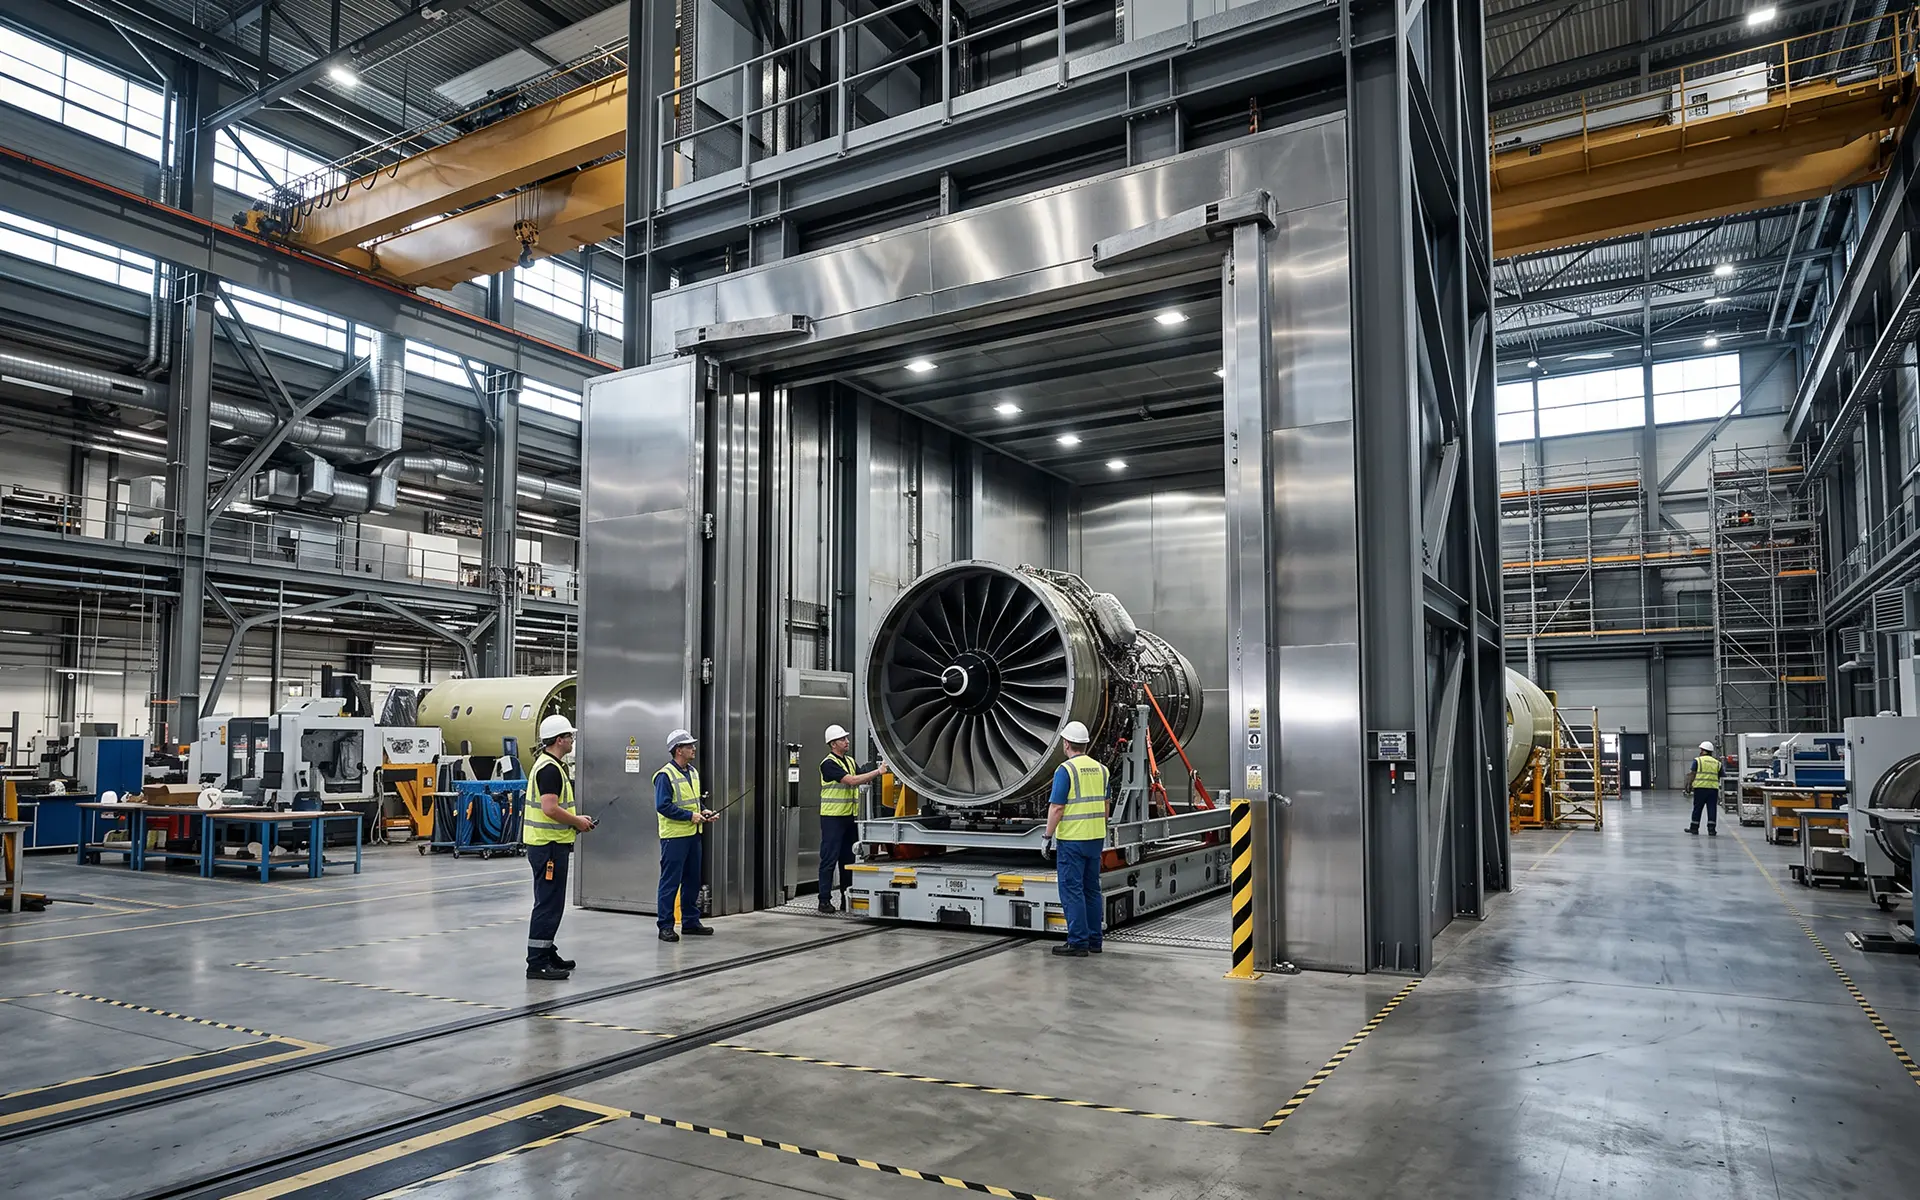
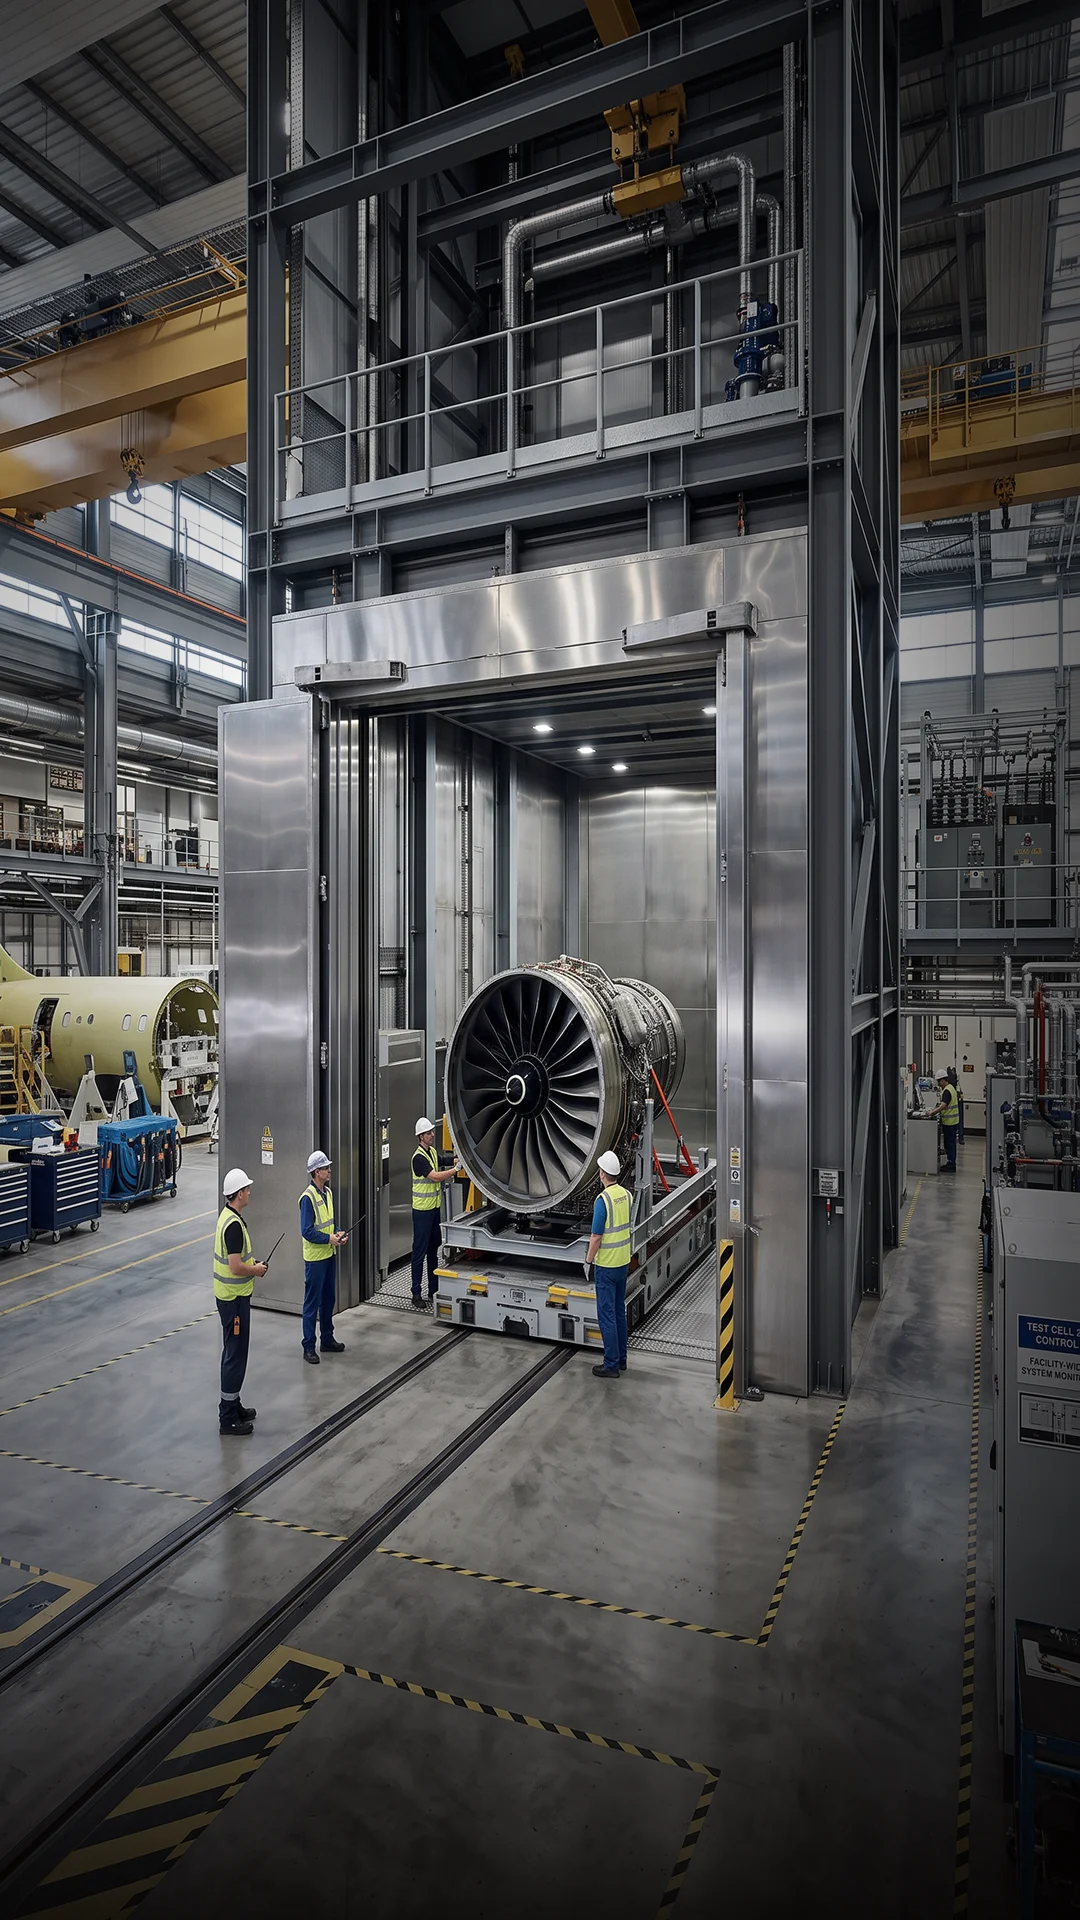
Industrial plants, chemical facilities, manufacturing units, warehouses, pharmaceutical facilities, food-processing plants and other specialized environments can demand elevator systems that go far beyond standard passenger or goods transportation.
Teknix Special Purpose Elevators are engineered around the environment, application and safety requirements of the project.
From explosion-risk areas and high-dust environments to applications requiring enhanced ingress protection, specialized materials or project-specific certifications, Teknix develops elevator solutions designed to perform reliably under demanding operating conditions.
Our approach combines elevator engineering, application-specific design, carefully selected components and controlled manufacturing to create solutions that are tailored to the requirements of each installation.
Special-purpose elevators can involve multiple standards and certification requirements depending on the application, country, hazardous-area classification and equipment involved.
Teknix evaluates the applicable requirements during the engineering stage rather than treating certification as an afterthought.
Where certification is required, the exact certification scope should be established based on the specific component, equipment, elevator configuration and application. This ensures that the documentation and certification correspond to the actual equipment being supplied.
 Chemical
 Oil & Gas
 Pharmaceutical
 Food & Beverages
 Manufacturing
 Warehousing & Logistics
 Cement & Minerals
 Power & Utilities
Every installation is approached around the specific environment and project requirements
Dust, moisture, chemicals, temperature and exposure conditions.
Usage, operating demands and project-specific requirements.
Components, finishes and equipment selected for the environment.
Relevant standards, protection requirements and certification considerations.